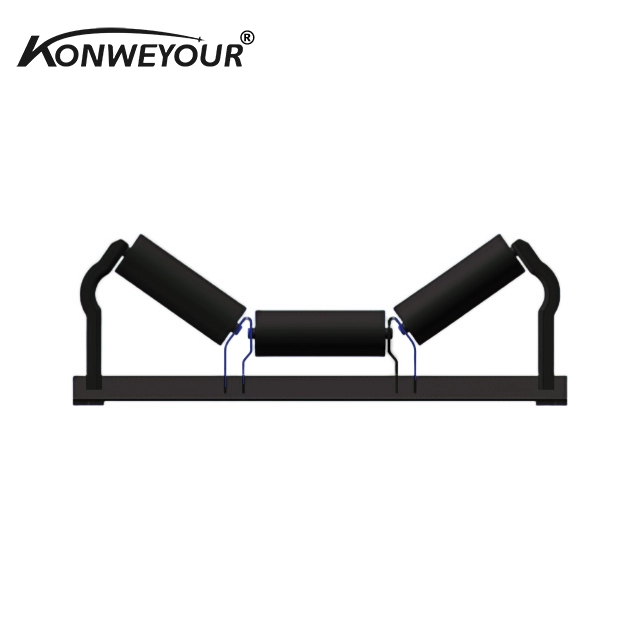
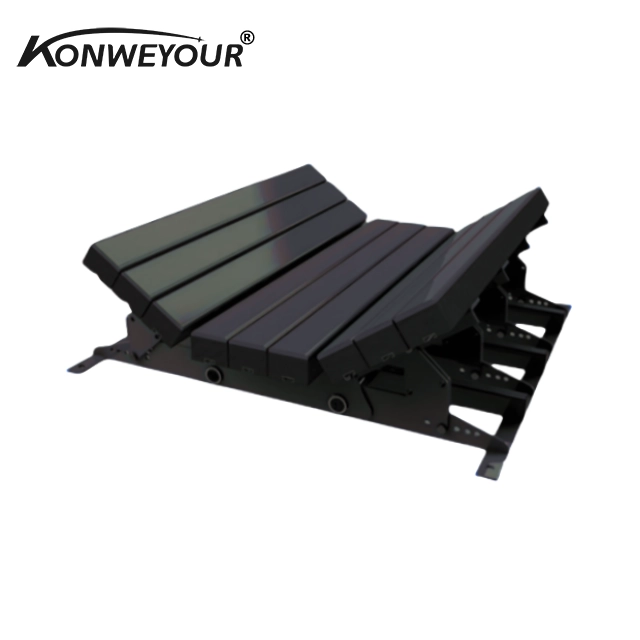
Precision-engineered spare parts ensuring maximum uptime for continuous industrial transport.
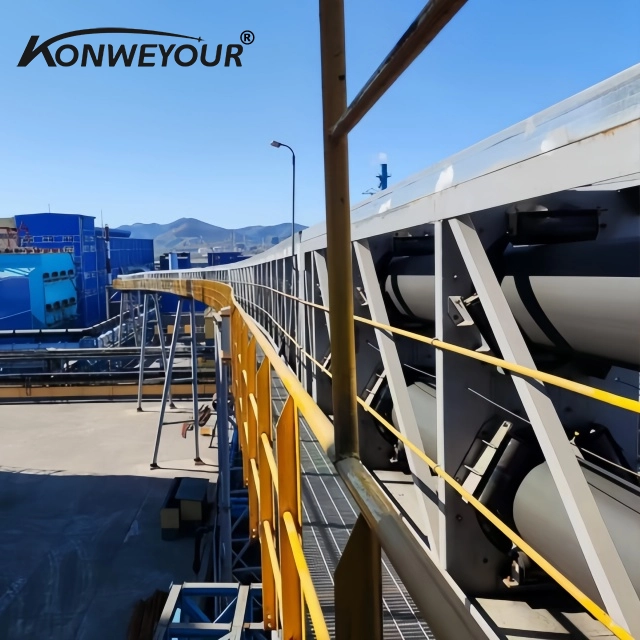
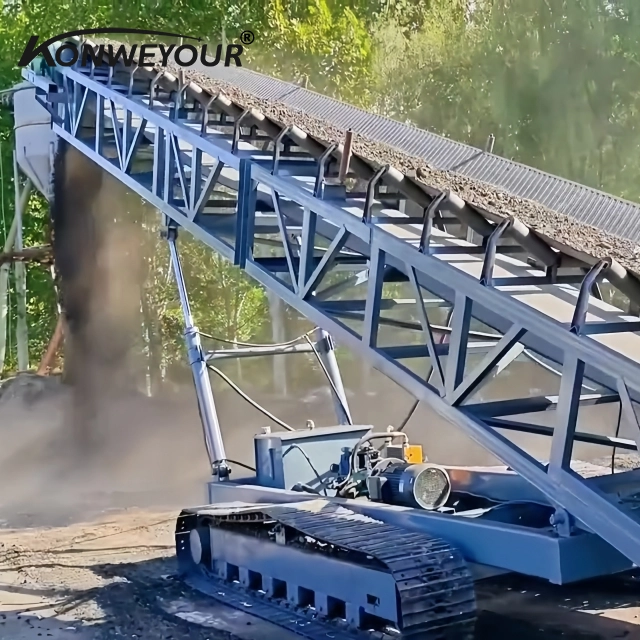
Focusing on durability, efficiency, and compliance with international mining standards.
In the South African industrial landscape, particularly within the coal and mineral extraction sectors, the reliability of a conveyor system is critical. The harsh environmental conditions and the abrasive nature of materials require equipment that minimizes friction and maximizes structural integrity.
Local operators prioritize low-maintenance components that can operate continuously under high loads. The shift toward energy-efficient transport is driving the demand for advanced rollers and pulleys that reduce power consumption across long-distance haulage routes.
Procurement decisions in this region are heavily influenced by the ability of the supplier to meet strict global technical specifications. Whether it is JIS or GB standards, the adaptability of manufacturing is a key differentiator for long-term operational success.
Integrating intelligent monitoring with robust hardware is becoming a necessity to prevent unplanned downtime, making the choice of high-grade conveyor components a strategic investment rather than a simple purchase.
From basic mechanical transport to intelligent, eco-friendly material ecosystems.
Focus on basic belt strength and simple pulley mechanisms for bulk transport.
Adoption of global standards like CEMA and DIN to ensure component interchangeability.
Introduction of high-impact beds and advanced belt cleaners to reduce wear.
Integration of sensors for real-time health monitoring of rollers and belts.
Development of energy-efficient, low-emission conveyor solutions for sustainable mining.
Transitioning from scheduled to condition-based maintenance using AI-driven diagnostics for conveyor idlers.
Implementing regenerative braking and low-friction components to lower the carbon footprint of mine sites.
Increasing use of prefabricated conveyor transfer systems for rapid deployment and easier upgrades.
Enhancing operational stability through technical innovation and quality control.
Utilizing wear-resistant materials in rollers and pulleys to extend the replacement cycle in abrasive environments.
Integrating impact beds and belt cleaners to prevent material spillage and reduce worker risk.
Rigorous adherence to ISO9001, CE, and TÜV certifications to guarantee global interoperability.
Designing seamless conveyor transfer systems that optimize material flow between stages.
The convergence of industry and academia has allowed for breakthroughs in energy-efficient conveyor designs. By collaborating with research institutes, the focus has shifted toward reducing the rolling resistance of idlers, which directly impacts the total cost of ownership for large-scale mining operations.
For South African enterprises, the ability to customize equipment to meet specific geological and material density requirements is paramount. A flexible manufacturing approach ensures that every pulley and belt is optimized for the specific tonnage and distance of the local project.
Practical implementations of conveying technology in South Africa's core industries.
Deployment of heavy-duty coal mine conveyor systems designed for high-volume throughput and abrasive resistance in deep-pit mining.
High-capacity conveyor transfer systems used in coastal ports to efficiently move minerals from storage silos to cargo vessels.
Continuous belt conveyors providing a steady flow of coal to boilers, featuring advanced belt cleaners to prevent residue build-up.
Reliable transport of cement and aggregates using customized rollers and pulleys tailored for construction plant environments.
Complex conveyor networks integrating impact beds at loading points to protect belts from large ore fragments during the crushing and screening process.
A journey of integration between R&D, manufacturing, and global service.
The company was established with a primary focus on the design, manufacturing, and installation of bulk material handling equipment.
Launched the first series of self-developed high-performance conveyor systems, establishing a reputation for quality and reliability.
Initiated exports to Southeast Asia, marking the beginning of a global strategy to serve international mining and industrial hubs.
Implemented modernized production lines and advanced manufacturing technologies to significantly increase annual output.
Successfully exported products to over 40 countries across Asia, Europe, Africa, and the Americas, becoming a trusted global supplier.
From precision rollers to durable pulleys, ensure your system operates at peak efficiency.
Expert answers to help you optimize your material handling infrastructure.
Partner with Hebei Juntong to implement durable, high-performance material handling solutions tailored to your specific industrial requirements.
Get a Customized Solution Now