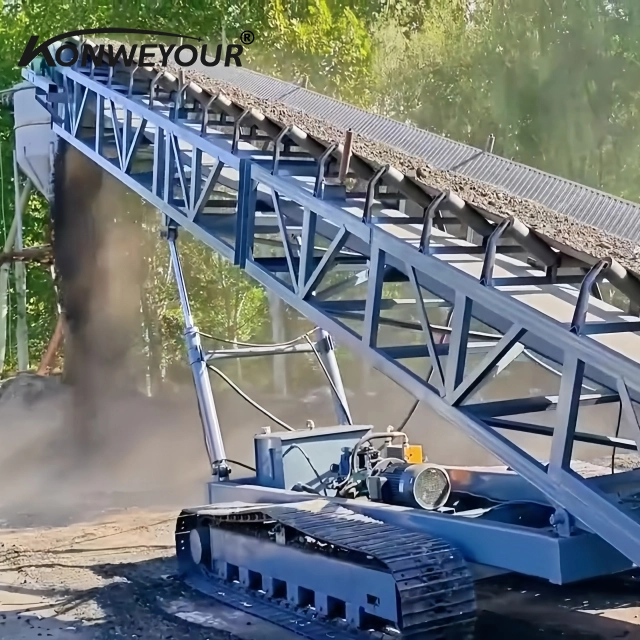
Providing a comprehensive range of high-reliability transport systems designed for mining, ports, and power plants to ensure seamless material flow.

Analyzing the intersection of resource wealth and logistical infrastructure requirements.
The Central African Republic possesses significant mineral potential, but the extraction process often faces hurdles due to rugged geographical conditions and a lack of integrated transport infrastructure. In the mining sector, the demand for a reliable mine conveyor is critical to bridge the gap between extraction points and processing facilities, reducing dependence on manual labor and inefficient trucking in remote areas.
Operational efficiency is often hampered by the harsh environment, which accelerates the wear and tear of mechanical parts. This creates a recurring need for high-quality conveyor components, such as heavy-duty rollers and idlers, that can withstand abrasive materials and fluctuating humidity. Local operators increasingly seek systems that prioritize durability over initial low cost to minimize unplanned downtime.
As the region looks toward diversifying its industrial base, there is a growing opportunity to implement integrated conveyor transfer systems. By upgrading from fragmented transport methods to continuous flowing systems, mining enterprises can significantly lower their operational costs per ton and improve the overall safety of their material handling ecosystems.
From basic mechanical belts to intelligent, energy-efficient material transport.
Reliance on simple belt systems with limited capacity and high maintenance requirements in mining sites.
Introduction of global standards like CEMA and DIN, allowing for larger capacities and better component interchangeability.
Integration of energy-saving drives and smart monitoring to optimize throughput and reduce carbon footprints.
Key drivers shaping the next generation of industrial conveying systems.
Reducing human intervention in hazardous mining zones through automated belt tensioning and smart start-stop sequences.
Utilizing high-performance polymers and treated alloys for rollers and belts to extend service life in abrasive environments.
Implementing prefabricated modules that allow for rapid installation and easy replacement of damaged sections in remote sites.
Focusing on dust suppression and noise reduction to meet evolving international environmental and safety standards.
The shift toward integrated digital twins and predictive maintenance is creating a new paradigm where downtime is forecasted rather than reacted to. For operators in Central African Republic, this means a significant increase in ROI as the lifespan of the entire conveyor system is maximized through precision care.
Global supply chain optimization now allows for the delivery of high-spec components that comply with CEMA and ISO standards, ensuring that local installations maintain the same reliability as those in developed industrial hubs.
Practical implementation of conveying technology across various operational environments.
Deploying heavy-duty coal mine conveyor systems to move massive volumes of ore from the pit to the surface, reducing fuel costs and increasing output consistency.
Utilizing high-capacity transfer systems for the loading and unloading of minerals, ensuring rapid turnaround for vessels and minimizing material spillage at the docks.
Implementing precise conveying systems for coal and biomass feed, ensuring a steady supply of fuel to boilers with integrated cleaning systems to prevent buildup.
Using specialized belts and idlers in cement and aggregate plants to transport abrasive raw materials without compromising belt integrity or motor life.
Integrating automated conveyor loops for the movement of bagged minerals or processed goods, streamlining the transition from production to dispatch.
The global growth and technical evolution of Hebei Juntong Machinery Manufacturing Co., Ltd.
Hebei Juntong Machinery Manufacturing Co., Ltd. was established with a focus on the design, manufacturing, and installation of bulk material handling equipment.
Launched the first series of high-performance conveyor systems, gaining strong recognition for quality and reliability in the domestic industrial market.
Expanded into Southeast Asia, marking the beginning of a global strategy to provide conveying solutions to diverse international markets.
Implemented advanced production lines and modernized manufacturing technologies to significantly increase annual capacity and efficiency.
Successfully exported equipment to over 40 countries across Asia, Europe, Africa, and the Americas, becoming a trusted global supplier.
Continuing investment in R&D to develop energy-efficient and eco-friendly conveyor solutions for evolving global industrial needs.
Explore our specialized range of precision-engineered spare parts and transfer systems designed for maximum durability and low maintenance.
Common inquiries regarding the deployment and maintenance of conveyor systems in challenging environments.
Partner with Hebei Juntong Machinery Manufacturing Co., Ltd. to implement durable, high-efficiency conveying solutions tailored to your specific industrial needs. Increase your operational uptime and lower costs today.
Get a Customized Solution