


Comprehensive range of industrial-grade conveyor components and complete transport systems designed for maximum uptime.
Addressing the unique environmental and operational challenges of the local mining and port infrastructure.
In the Asia - Philippines region, the material handling industry is heavily influenced by high humidity and the corrosive nature of coastal mining environments. Consequently, local operators prioritize corrosion resistance and structural durability when procuring a coal mine conveyor, as equipment failure in remote sites leads to significant operational downtime.
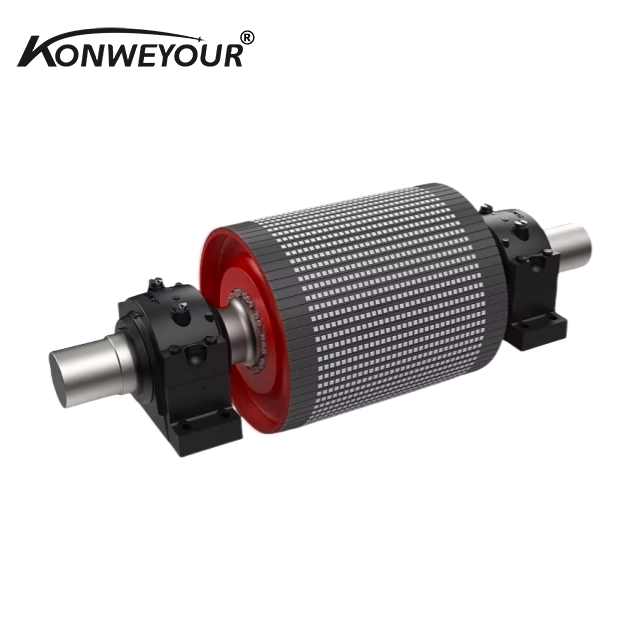
Procurement decisions in this market are increasingly shifting toward total cost of ownership (TCO) rather than initial capital expenditure. This means there is a growing demand for high-performance rollers and pulleys that extend the replacement cycle.
Supply chain stability is a critical factor for Philippine industrial sites. The ability to source components that comply with international standards such as JIS or CEMA ensures that systems can be maintained using globally recognized technical specifications.
Furthermore, the integration of energy-efficient drive systems is becoming a priority to reduce operational costs in power-intensive mining and building material plants across the archipelago.
Tracing the shift from simple mechanical transport to intelligent, energy-efficient ecosystems.
Focus on basic belt tension and gravity-fed material transport systems.
Adoption of CEMA and DIN standards to ensure component interchangeability.
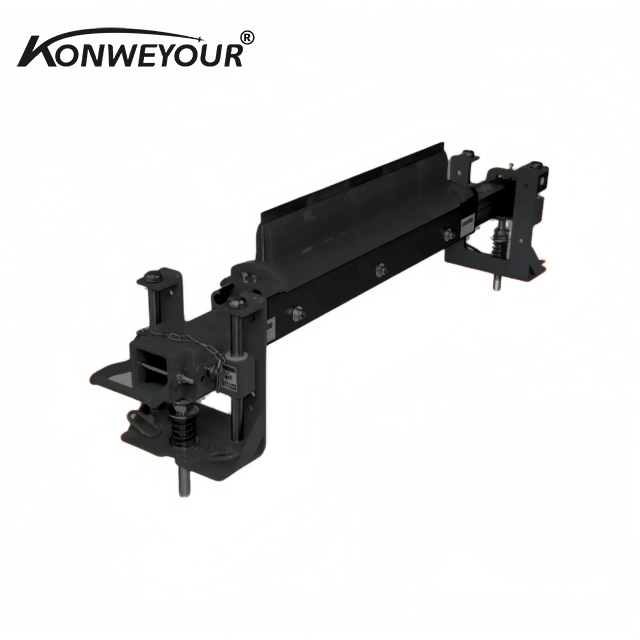
Introduction of high-impact beds and advanced belt cleaners to reduce wear.
Integration of sensors for real-time monitoring of conveyor health and alignment.
Focus on low-friction components and energy-saving drive technologies.
Transitioning from scheduled replacements to condition-based monitoring using AI to predict bearing failures in rollers.
Increased use of conveyor transfer systems that allow for rapid reconfiguration of plant layouts.
Developing belt materials and components that reduce environmental impact and energy consumption during transit.
How precision engineering solves the most persistent challenges in industrial conveying.
Using advanced heat treatment and precision machining for pulleys and idlers to maximize operational life.
Designing seals and coatings specifically for the high-sulfur and high-moisture environments of mine sites.
Flexible manufacturing that adheres to CEMA, DIN, JIS, and GB specifications for global compatibility.
Providing a full ecosystem from belt cleaners and impact beds to complete conveyor system design.
The primary technical challenge in bulk handling is managing the transition points where material drops from one conveyor to another. Without proper impact beds and alignment, belts suffer from premature wear and misalignment.
By integrating research with industrial application, modern systems now utilize intelligent energy-saving technologies that reduce the carbon footprint of the entire material transportation ecosystem.
Tailoring conveying technology to specific industrial environments and material types.
High-capacity belt conveyors designed to move heavy ores across rugged terrains, requiring reinforced pulleys and high-strength belts to handle abrasive materials.
Corrosion-resistant conveyor components for transferring minerals from mine-site transport to shipping vessels in saline environments.
Specialized coal mine conveyor systems focusing on dust suppression and efficient transfer for consistent fuel supply.
Heavy-duty transfer systems for limestone and clinker, utilizing impact beds to prevent belt damage during high-drop loading phases.
Hygenic and efficient conveyor systems for transporting grains or processed agricultural products, emphasizing low-friction rollers and easy-clean components.
A global provider of integrated conveying system research, development, and manufacturing.
Established with a core focus on the design, manufacturing, sales, and installation of bulk material handling and conveying equipment.
Launched the first series of self-developed high-performance conveyor systems, achieving strong recognition for quality and reliability.
Began exploring overseas markets with the first batch of products exported to Southeast Asia, marking the start of internationalization.
Implemented advanced manufacturing technologies and modernized production lines to increase annual capacity and efficiency.
Products successfully exported to over 40 countries across Asia, Europe, Africa, the Americas, and the Middle East.
From conveyor idlers and rollers to impact beds and belt cleaners, we provide full-process quality control for every component.
Professional answers to help you make the right technical and procurement decisions.
Partner with Hebei Juntong Machinery to implement reliable, standard-compliant conveying solutions for your manufacturing and mining projects.
Request Your Custom Solution