


Integrating robust engineering with flexible manufacturing to deliver high-performance conveying equipment tailored to UK technical specifications.

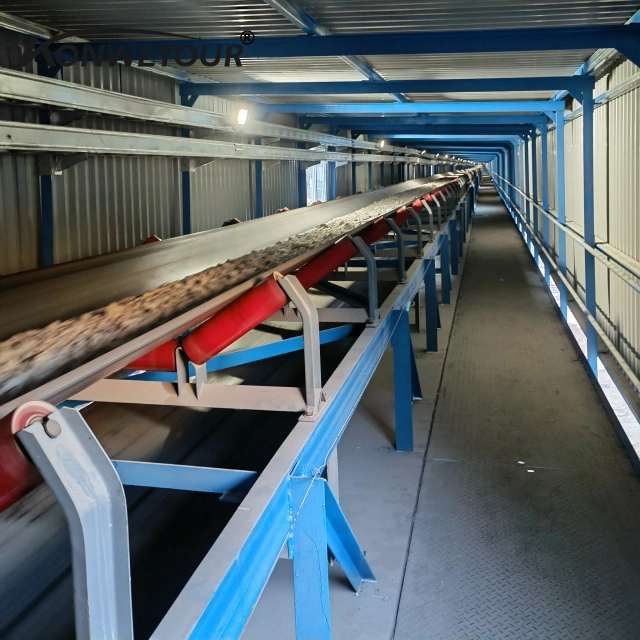
Addressing the rigorous demands of British industrial transportation and resource extraction.
The United Kingdom's industrial landscape, particularly in resource extraction and heavy manufacturing, requires conveying systems that can withstand high load capacities while adhering to strict safety and environmental regulations. Local operations often face the challenge of integrating new technology into aging infrastructure, making the demand for versatile and high-durability equipment a priority for maintaining competitive productivity.
Operational efficiency in the UK is currently focused on reducing energy consumption and minimizing downtime. For those managing a coal mine conveyor or similar bulk handling systems, the primary challenge lies in the wear and tear of critical components. The adoption of precision-engineered rollers and pulleys is essential to lower friction and extend the service life of the entire transport line.
Looking forward, the UK market is shifting toward "intelligent conveying," where energy-efficient motors and sensor-based monitoring are integrated into the system. There is a significant opportunity for enterprises to transition toward modular conveyor transfer systems that allow for rapid reconfiguration and easier maintenance, ensuring that material flow remains uninterrupted regardless of site complexity.
Tracing the transition from mechanical simplicity to intelligent industrial ecosystems.
Focus on basic structural strength and manual operation for heavy bulk transport in early industrial sites.
Introduction of global standards like DIN and CEMA, improving the interchangeability of conveyor components.
Integration of energy-saving technologies and smart sensors for real-time monitoring and predictive maintenance.
Analyzing the technical and commercial vectors driving the future of material handling.
Development of low-rolling-resistance idlers and energy-efficient drive systems to cut operational costs.
Use of advanced composite polymers and treated steels to combat corrosion in humid UK environments.
Shifting from reactive repairs to data-driven maintenance using integrated sensor networks.
Designing systems that can be expanded or modified without requiring a total infrastructure overhaul.
The future of the conveying industry lies in the intersection of mechanical robustness and digital intelligence. As UK industries strive for higher sustainability ratings, the demand for "green" conveying solutions—those that minimize waste and maximize energy efficiency—will continue to grow, creating a high-value market for customized engineering.
Supply chain resilience is also becoming a key factor. Companies are increasingly looking for partners who can provide a full spectrum of parts, from core hosts to precision spare parts, ensuring that maintenance doesn't depend on a fragmented group of suppliers.
Deploying specialized conveying solutions across diverse UK economic sectors.
Utilizing heavy-duty belt conveyors and impact beds to handle abrasive ores in Northern English quarries, ensuring maximum uptime in harsh environments.
Implementing high-capacity transfer systems for bulk cargo handling in UK ports, optimizing the flow between ships and storage silos.
Deploying reliable conveyor rollers and belt cleaners to ensure a steady stream of fuel materials, minimizing residue and preventing system blockages.
Integrating precise conveyor pulleys and belt systems in cement and brick plants to automate the movement of raw materials through production lines.
Installing modular conveyor components to streamline sorting and dispatch processes in large-scale UK logistics hubs, increasing throughput speed.
Hebei Juntong Machinery Manufacturing Co., Ltd.'s Global Development Journey
Established as a specialist in the design, manufacturing, and installation of bulk material handling and conveying equipment.
Launched self-developed high-performance conveyor systems, gaining strong recognition for quality and reliability.
Began exporting high-grade conveying solutions to Southeast Asia, marking the start of a global expansion strategy.
Implemented advanced production lines and technologies to significantly increase annual capacity and efficiency.
Successfully exported to over 40 countries across Asia, Europe, Africa, and the Americas as a trusted supplier.
Continuous investment in R&D for energy-efficient and eco-friendly conveyor solutions for a greener industrial future.
Providing a full range of certified spare parts to ensure the longevity and efficiency of your industrial transport ecosystem.
Expert answers to common questions regarding the deployment of conveyor systems in the UK.
Leverage our global manufacturing expertise and certified quality to build a more efficient, durable, and low-consumption material transport ecosystem in the United Kingdom.
Get Professional Technical Quote