Understanding Motorized Conveyor Pulleys: Benefits, Applications & Market Trends
Motorized Conveyor Pulleys is a key solution in the industry, specifically within material handling and bulk processing sectors. This article explores how https://www.jtconveyor.com supports professionals with durable, high-performance products, and explains why this product is an ideal choice for businesses in these sectors.
Table of Contents
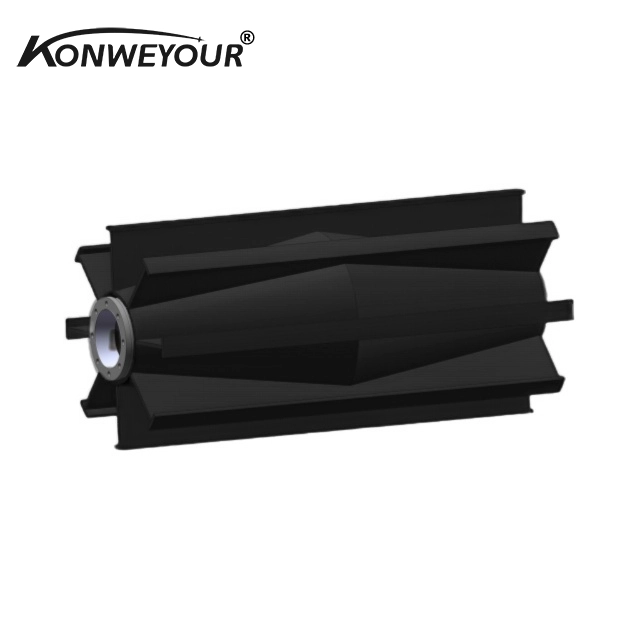
Motorized conveyor pulleys, frankly, feel like the quiet workhorses of many industrial setups. Fundamentally, they’re conveyor rollers integrated with an internal motor, eliminating the need for external drives or complicated belts. This streamlined design reduces the footprint and increases reliability — two things every plant manager dreams of. Technically speaking, these pulleys combine a steel shell, bearings, a sealed electric motor, and sometimes advanced control electronics, all engineered to drive the conveyor belt directly.
Compact design that reduces energy loss and maintenance points.
Available in torque capacities from 100 Nm up to 1500 Nm depending on model.
Case study: A bulk materials handler upgraded to JT Conveyor’s motorized pulleys saw a 30% reduction in downtime due to less belt slippage and easier repairs.
| Specification | Typical Range | Remarks |
|---|
| Diameter | 200 - 400 mm | Match conveyor belt width |
| Torque | 100 - 1500 Nm | Based on motor size/specs |
| Power Supply | 3-phase, 380-480 V | Industry standard |
| Speed | Variable, up to 65 m/min | Adjustable depending on control |
| IP Rating | IP66 or better | Water and dust resistant |
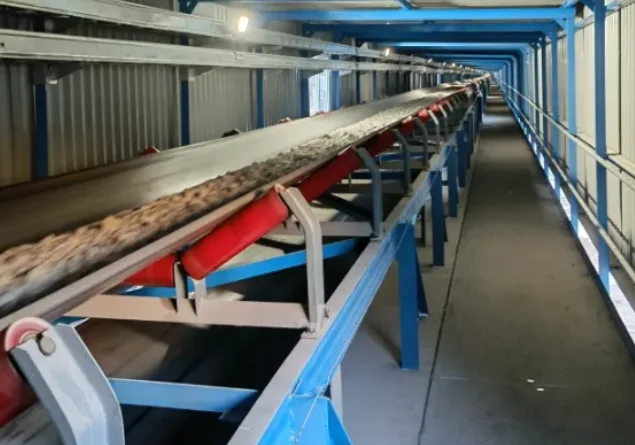
The range of industries leveraging these motorized conveyor pulleys is broader than you might expect — mining, food processing, packaging, and recycling all benefit. The integrated motor means fewer external components that can fail, because external drives and belts are replaced by a self-contained unit. Features like sealed-for-life bearings and vibration-resistant motors keep maintenance crews happier, too. Oddly enough, many engineers note how this simplification leads to faster system startups and smoother operation — which translates directly into uptime and throughput.
Ideal for harsh environments due to sealed designs and corrosion-resistant coatings.
Energy efficient; direct drive cuts power losses.
Supports modular conveyor designs, making expansions and upgrades smoother.
Cost, Maintenance & User Experience
Cost-wise, motorized conveyor pulleys might look like a significant upfront investment compared to conventional pulleys with external gearboxes. However, when you factor in the total cost of ownership—the reduced maintenance, minimized downtime, and extended belt life—it’s a different picture. I’ve heard many plant operators say the ROI hits within two years due to these savings. Plus, the simplicity of design means technicians generally find repairs and diagnostics less stressful.
Reduced number of moving parts means less frequent breakdowns.
Energy-saving motors cut electrical bills over time.
Positive testimonials from mining companies emphasize resilience under heavy load.
Sustainability & Market Trends
Sustainability has become a buzzword, sure, but in the context of conveyor technology, it’s about real, measurable gains. Motorized conveyor pulleys, with their energy-efficient motors and long-lasting components, reduce waste and power consumption — which aligns with many industries’ carbon footprint goals. Regulatory bodies are increasingly nudging manufacturers toward greener practices, and options like variable speed drives further reduce excess power drain. Market trends show steady growth in demand, particularly in regions automating logistics and warehousing.
| Vendor | Product Range | Durability | Customization | Lead Time |
|---|
| JT Conveyor | 100+ Models | High — Steel shell, sealed bearings | Full bespoke options | 4-6 weeks |
| Vendor A | 50 Models | Medium | Limited | 6-8 weeks |
| Vendor B | 80 Models | High | Moderate | 5-7 weeks |
Frequently Asked Questions about Motorized Conveyor Pulleys
- What is Motorized Conveyor Pulleys and how does it work?
- Simply put, a motorized conveyor pulley is a conveyor roller with a built-in electric motor that directly drives the conveyor belt. Instead of using a separate motor and gearbox connected by belts or chains, everything’s sealed inside the pulley shell. When powered, the motor rotates the pulley, moving the belt and materials along.
- What are the main benefits of using Motorized Conveyor Pulleys in industrial applications?
- They reduce maintenance because there are fewer moving parts exposed to wear, increase energy efficiency by eliminating power losses in belts, and improve system reliability. Plus, their compact design frees up installation space and simplifies conveyor layouts.
- How does Motorized Conveyor Pulleys compare to traditional alternatives?
- Compared to conventional pulleys with external motors, motorized pulleys offer a cleaner, simpler solution. They eliminate belts and gearboxes, which are prone to slipping and require frequent adjustment. This leads to fewer breakdowns and often better energy consumption.
- What industries can benefit most from Motorized Conveyor Pulleys implementation?
- Primarily mining, bulk materials handling, food and beverage processing, packaging, recycling, and warehousing are sectors that see significant gains. For example, a recycling plant reduced downtime considerably after switching to motorized pulleys.
Conclusion on Motorized Conveyor Pulleys from china
To wrap up: motorized conveyor pulleys represent a smart investment for businesses aiming to boost efficiency while cutting maintenance headaches. The integration of motor and pulley in one rugged unit offers practical advantages in uptime, energy saving, and system simplicity. And if you’re interested in exploring trusted options, visit our website. It's pretty clear that their range and track record make them a solid choice.
Reflecting on the growing adoption of motorized conveyor pulleys, it feels like an elegant evolution in conveyor tech — marrying efficiency with simplicity. For anyone curious, this is definitely a topic to watch as automation and sustainability continue to drive industrial innovations.
References:
ISO 5048: Mechanical conveyor drives – Design and performance guidelines.
Industry case studies on JT Conveyor product line, 2023.
Market analysis reports on conveyor automation, 2024.