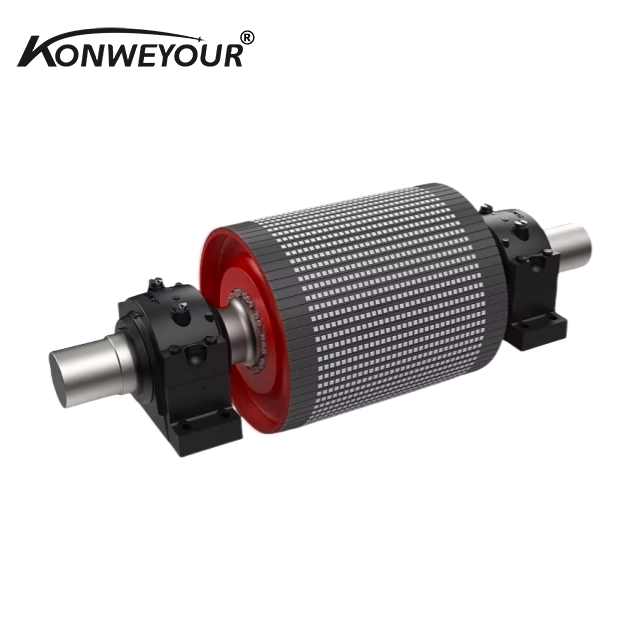
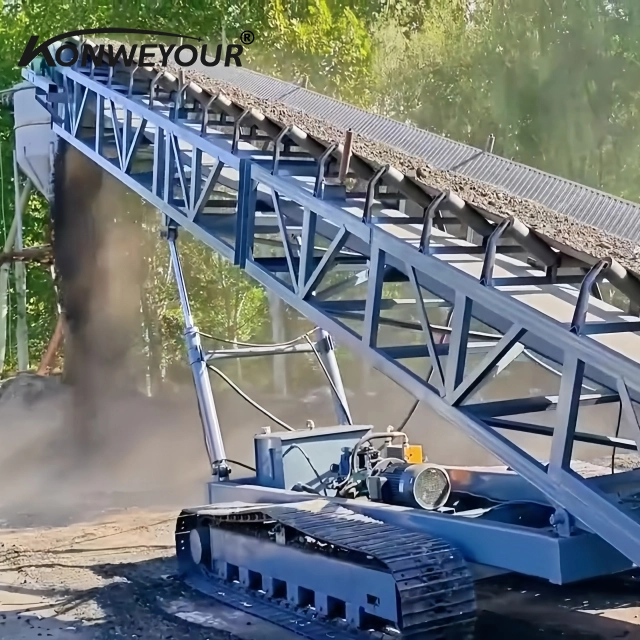
High-precision spare parts engineered to meet CEMA, DIN, JIS, and GB standards for maximum durability.

Addressing the unique logistical challenges of bulk material transport in Caribbean industrial environments.
In North America - Cuba, the demand for a robust mine conveyor is driven by the need to modernize aging infrastructure in the mining and port sectors. High humidity and saline coastal air make corrosion resistance a primary concern for local procurement officers, necessitating the use of advanced materials and precision-engineered rollers.
Operations in this region prioritize equipment that minimizes downtime and reduces energy consumption, as operational efficiency directly impacts the cost-effectiveness of bulk material extraction and transport.
The shift toward integrated conveyor transfer systems allows Cuban industrial sites to optimize the transition points between different conveyor belts, reducing spillage and wear on belt cleaners and impact beds.
Consequently, there is a growing trend toward selecting suppliers who can provide a full ecosystem of spare parts, from idlers to pulleys, ensuring seamless compatibility and simplified maintenance cycles.
From mechanical transport to intelligent, energy-efficient ecosystems.
Focus on basic belt strength and structural stability for bulk hauling.
Adoption of international standards like CEMA and DIN for interchangeable parts.
Introduction of advanced impact beds and belt cleaners to extend equipment life.
Integration of sensors for real-time condition monitoring of idlers and rollers.
Focus on low-friction components to reduce total operational energy consumption.
Developing sustainable materials for conveyor belts and rollers to reduce the environmental footprint of mining operations.
Moving from scheduled replacements to AI-driven predictive maintenance based on real-time component wear data.
Increased adoption of modular conveyor transfer systems that can be quickly reconfigured for different site layouts.
How engineering breakthroughs are solving traditional material handling bottlenecks.
Reducing the coefficient of friction in conveyor idlers to lower electricity costs and motor strain.
Applying advanced coatings to conveyor components to withstand saline and humid Caribbean climates.
Integrating heavy-duty impact beds at loading points to prevent belt puncture and extend belt lifespan.
Designing optimized transfer chutes to ensure smooth material flow and reduce dust emission.
Technical specifications are no longer one-size-fits-all. The integration of industry, academia, and research allows for the creation of conveyor systems that are tailored to the specific density and abrasiveness of the materials being moved, whether it be coal, ore, or building materials.
By focusing on the synergy between the drive system and the support components—such as pulleys and rollers—companies can achieve a significant reduction in total cost of ownership (TCO) while increasing overall system availability.
Tailored material handling solutions for diverse industrial environments.
Deployment of heavy-duty coal mine conveyor systems to handle high-volume ore transport under harsh outdoor conditions.
High-capacity belt conveyors and transfer systems for the efficient loading and unloading of mineral exports at Caribbean ports.
Precision conveying of limestone and clinker using specialized rollers and pulleys to ensure continuous plant operation.
Implementing reliable conveyor components to ensure a steady supply of fuel to boilers with minimal dust and leakage.
Customized light-to-medium duty conveyor systems for the internal movement of bagged materials and industrial components within logistics hubs.
A legacy of engineering excellence in industrial conveying solutions.
Founded with a core focus on the design, manufacturing, sales, and installation of bulk material handling and conveying equipment.
Launched the first series of self-developed high-performance conveyor systems, gaining recognition for reliability.
Began exporting to Southeast Asia, marking the strategic shift towards becoming a global supplier.
Implemented advanced manufacturing technologies and modernized production lines to increase capacity.
Successfully exported to over 40 countries across Asia, Europe, Africa, and the Americas.
From core host systems to precision spare parts, we empower global customers with efficient and long-life industrial transportation.
Technical and procurement guidance for industrial conveying systems.
Discover how Hebei Juntong's specialized manufacturing in the continuous conveying equipment sector can reduce your operational costs and increase system reliability.
Get a Customized Solution