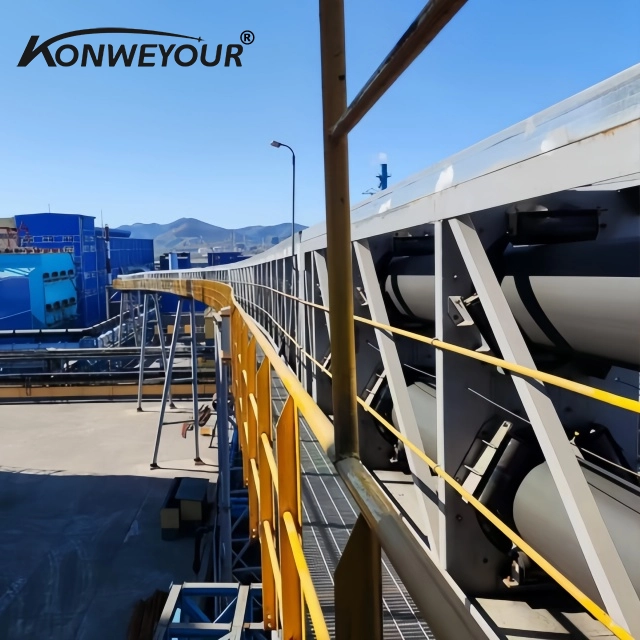
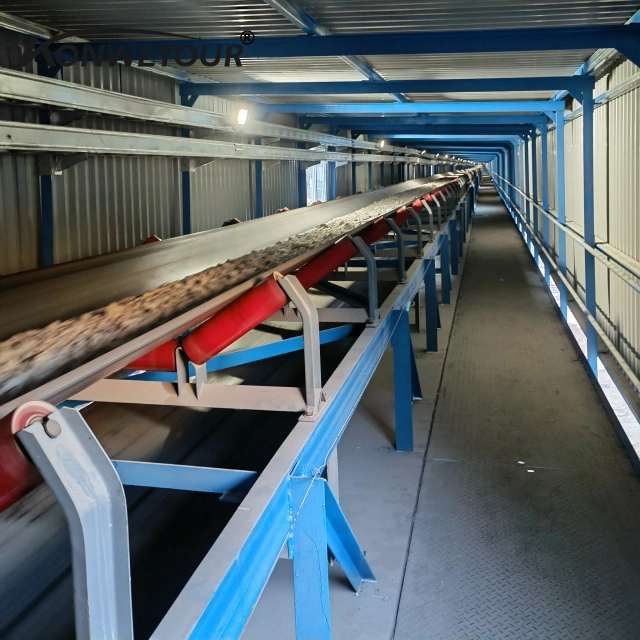
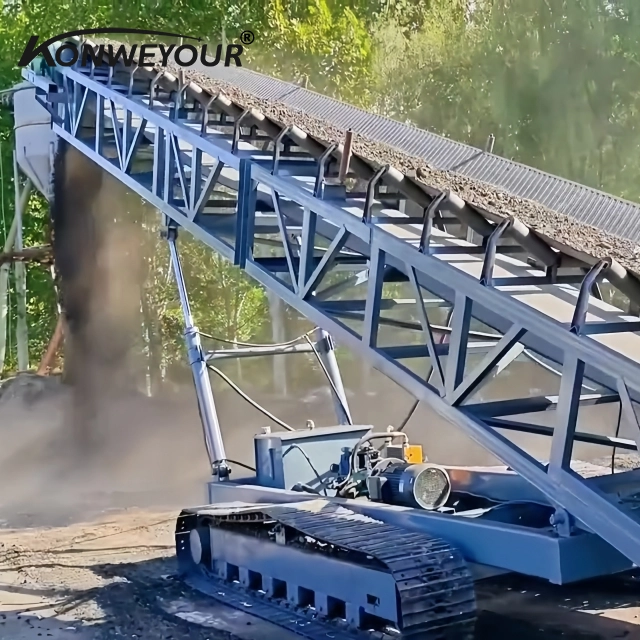
Looking for high-performance tubular material handling? As leading China suppliers and a professional factory, we provide Wear Resistant Pipe Rubber Conveyor Belts designed to eliminate spillage and dust. Ideal for mining and chemical industries, our durable belts ensure safe, enclosed transport over long distances with minimal maintenance.
The Wear Resistant Pipe Rubber Conveyor Belt is a cutting-edge material handling solution engineered for the most demanding industrial environments. Featuring a unique, fully enclosed tubular structure, this conveyor system eliminates material spillage and suppresses dust emissions, ensuring a clean, safe, and environmentally compliant operational workspace.
Constructed from premium-grade wear-resistant rubber compounds and reinforced with high-strength fabric or steel cord carcasses, our pipe belts are designed for superior tensile strength and durability. Whether transporting bulk materials over long distances or operating in corrosive conditions, this system delivers unmatched reliability and stability for heavy-duty industrial applications.
| Structure Type | Fully Enclosed Tubular Shape | Belt Material | Premium Wear-Resistant Rubber |
|---|---|---|---|
| Carcass Reinforcement | High-Strength Fabric / Steel Cord | Wear Resistance | High Abrasion Resistance Grade |
| Environmental Protection | Dust-Proof & Leak-Proof | Weather Resistance | Corrosion & Moisture Resistant |
| Load Capacity | Heavy-Duty / High Tensile | Application Range | Mining, Cement, Chemical, Power |
| Maintenance Level | Low Maintenance Design | Operational Stability | High-Stability Long Distance |
The tubular structure ensures fully enclosed transportation, preventing material scattering and dust pollution.
High-quality rubber compounds provide exceptional anti-wear capacity, reducing replacement frequency.
Reinforced steel wire or canvas cores support heavy-load and ultra-long distance conveying needs.
Effective resistance to moisture, corrosion, and harsh climates ensures smooth year-round operation.
Robust engineering minimizes wear and tear, significantly lowering downtime and operational costs.
Optimized for cement plants, mining sites, and chemical facilities requiring safe closed systems.

Real-time tracking of conveyor belt stocks and components for rapid deployment.
Advanced monitoring of belt tension and wear levels to prevent unexpected failures.
Automated scheduling and notification for routine inspections and rubber health checks.
Integrated reporting tools to ensure dust emission standards and safety protocols are met.
Seamless coordination between production and shipping for large-scale conveyor projects.
Data-driven adjustments to conveyor speed and load to maximize energy efficiency.
| Feature | Standard Open Belt | Pipe Rubber Conveyor |
|---|---|---|
| Material Loss | High (Spillage) | Near Zero (Enclosed) |
| Environmental Cost | High (Dust Control) | Low (Self-contained) |
| Maintenance Cycle | Frequent Repairs | Extended Intervals |
| Service Lifespan | Moderate | High (Wear-Resistant) |
| Operational Safety | Risk of Leakage | Maximum Protection |
The primary benefits include a fully enclosed transport system that prevents material spillage and dust emission, higher protection against weather, and a reduced environmental footprint.
It is ideal for bulk materials in the mining, cement, and chemical industries, especially those that are dusty, prone to leaking, or sensitive to moisture.
The use of high-strength fabric or steel cord carcasses significantly increases the tensile strength, allowing the belt to handle heavy loads over long distances without stretching.
Yes, our belts are manufactured with premium rubber covers specifically designed to resist corrosion and moisture, making them suitable for chemical plant operations.
Due to the robust wear-resistant rubber and reinforced design, maintenance intervals are significantly longer compared to standard belts, reducing total cost of ownership.
Absolutely. The weather-resistant rubber covering protects the internal carcass from UV rays, extreme temperatures, and moisture, ensuring stable operation worldwide.

Jun 03,26
Premium Durable Industrial Conveyor Belt Material for Sale

Oct 23,26
Choosing a Rubber Coated Return Roller: Medium, Dimensions and Operating Conditions
Nov 11,25
The Evolution and Essential Role of Modern Conveyor Systems
From rudimentary wooden rollers in ancient mines to the sophisticated, AI-driven networks that power global logistics, the evolution of the conveyor system marks a pivotal chapter in industrial history.
Jan 26,26
Understanding Modern Trends in Conveying Equipment Manufacturer and Design
Nov 11,25
Unearthing Efficiency: The Pivotal Role of Coal Mine Conveyor Systems
In the relentless pursuit of extracting vital resources, the efficiency and safety of material handling systems stand paramount.
Mar 10,26
Understanding the Benefits of Composite Conveyor Rollers for Efficient Material Handling
SUBSCRIBE NEWSLETTER