Heavy-duty machinery and spare parts designed to meet CEMA, DIN, and JIS standards for maximum reliability.


Balancing traditional extractive industries with modern efficiency requirements.
The Spanish industrial sector is currently shifting toward higher automation in bulk material handling. In regions with significant mining activities, there is a critical demand for mine conveyor systems that can handle abrasive materials while reducing energy consumption.
Procurement teams in Spain are increasingly prioritizing long-term lifecycle costs over initial purchase price, seeking components that offer superior wear resistance and reduced maintenance intervals to minimize operational downtime.
Operational efficiency in Spanish plants is heavily influenced by strict EU environmental and safety regulations. Compliance with CE and ISO standards is a non-negotiable requirement for any conveyor transfer systems deployed in the region.
CE Certification, Energy Efficiency, and Standardized Component Interoperability (DIN/CEMA).
From basic belt transportation to intelligent, integrated logistics ecosystems.
Focus on basic structural integrity and the adoption of global standards like DIN and CEMA to ensure part compatibility.
Development of specialized coal mine conveyor systems designed for high-impact and abrasive environments.
Integration of energy-efficient motors and smart monitoring to create sustainable, low-consumption transportation ecosystems.
Shift toward interchangeable conveyor components to reduce lead times for spare parts.
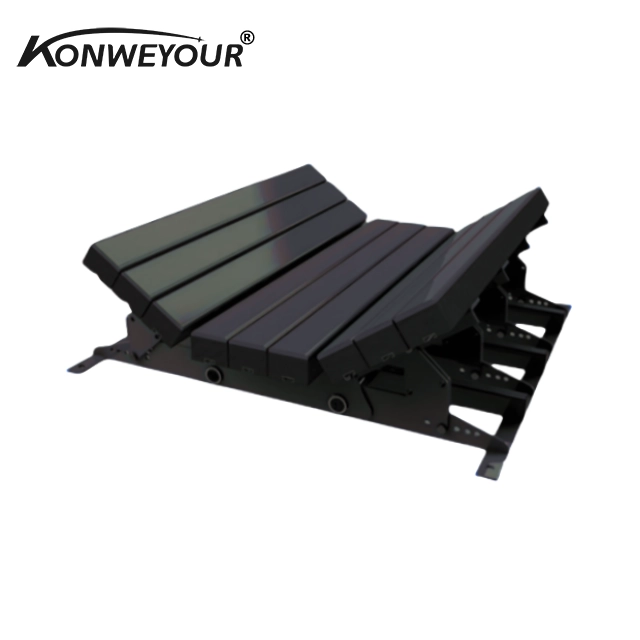
Implementation of advanced belt cleaners and impact beds to reduce material waste and energy loss.
Strict adherence to SGS, BV, and TUV certifications to facilitate seamless cross-border industrial deployment.
How technology is redefining the efficiency of industrial transportation.
Using sensor data to monitor roller and pulley wear, preventing catastrophic failures before they occur.
Developing low-friction conveyor rollers and optimized drive systems to cut operational electricity costs.
Automated transfer systems that adjust speeds based on real-time material load and flow requirements.
Adopting high-durability, recyclable polymers for belt cleaners and impact beds to reduce environmental impact.
The convergence of IoT and mechanical engineering is transforming the role of the conveyor from a simple transport tool to a data-generating asset. This allows operators to optimize the entire supply chain from the extraction point to the loading port.
As Spain continues to integrate more sustainable practices into its industrial base, the focus is shifting toward "green conveying"—reducing carbon footprints through higher mechanical efficiency and intelligent power management.
Tailored solutions for diverse geological and industrial environments.
Deploying heavy-duty belt conveyors with high-impact beds to handle raw ores in rugged terrains, ensuring stable flow to processing plants.
Installing specialized coal mine conveyor systems with integrated dust suppression and belt cleaners for environmental compliance.
Utilizing high-capacity conveyor transfer systems to move building materials and minerals from storage silos to shipping vessels.
Implementing precision rollers and pulleys to transport limestone and clinker through various production stages with minimal slippage.
Integrating reliable conveying components to ensure a continuous, uninterrupted supply of fuel to boilers in energy facilities.
A global provider of integrated industrial conveying solutions.
Hebei Juntong Machinery Manufacturing Co., Ltd. was founded with a focus on the design, manufacturing, and installation of bulk material handling equipment.
Launched a series of self-developed high-performance conveyor systems, gaining widespread recognition for reliability and durability.
Began exporting to Southeast Asia and beyond, adapting manufacturing capabilities to comply with diverse national standards.
Implemented modernized production technology to significantly increase annual capacity and precision in spare part manufacturing.
Successfully expanded into Europe, Africa, and the Americas, becoming a trusted supplier of conveyor rollers, pulleys, and belts.
Established technology laboratories with top research institutes to develop energy-efficient and intelligent conveyor ecosystems.
Explore our full range of high-reliability components including idlers, pulleys, and impact beds.
Expert answers regarding the selection and operation of conveying systems.
Contact our engineering team to discuss tailored conveyor solutions that meet strict European standards and enhance your operational efficiency.
Request a Technical Consultation