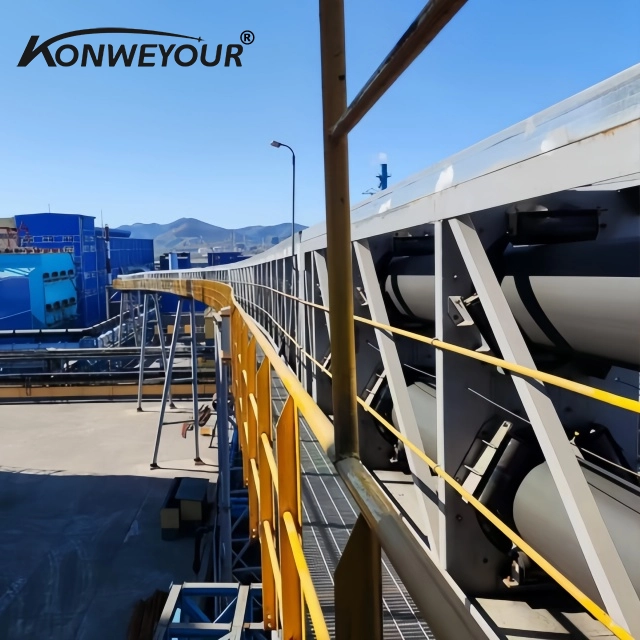



Specialized components designed to withstand the demanding environments of African mineral extraction.

Balancing high-volume throughput with equipment longevity in tropical and subterranean environments.
Zambia's economy is heavily anchored by its mining industry, particularly in the Copperbelt and North-Western provinces. The transport of raw ores requires a robust mine conveyor capable of handling abrasive materials over long distances. Local operations face unique challenges, including high humidity and fluctuating geological stability, which accelerate the wear and tear of mechanical parts.
To maintain operational continuity, procurement teams are shifting from generic replacements to precision-engineered conveyor components. The focus has moved toward reducing downtime by implementing high-reliability idlers and pulleys that conform to international standards like CEMA and DIN, ensuring compatibility with existing global infrastructure.
For engineers in Zambia, this means prioritizing impact resistance and corrosion protection. Selecting a supplier that integrates R&D with manufacturing allows for the customization of belt cleaners and impact beds specifically for the density and moisture content of local minerals, directly impacting the overall cost per ton of transported material.
From manual hauling to energy-efficient automated systems.
Emphasis on basic durability and manual belt adjustments with high maintenance intervals.
Adoption of global standards like JIS and GB to improve the interchangeability of spare parts.
Integration of low-friction rollers and intelligent monitoring to reduce power consumption.
Moving from reactive repairs to sensor-based monitoring of conveyor transfer systems to prevent catastrophic failure.
Increasing demand for modular components that allow rapid expansion of mine sites without full system redesigns.
Adopting belts and cleaners that reduce material spillage, minimizing environmental impact on surrounding landscapes.
Preparing for the next decade of resource extraction.
Integration of PLC controls for automated speed adjustment based on load volume.
New alloy coatings for rollers to extend lifespan in highly abrasive coal and copper mines.
Using virtual modeling to optimize the layout of coal mine conveyor paths before installation.
Implementing regenerative braking systems on downhill conveyor sections to recover power.
As Zambian mines venture deeper, the technical requirements for conveyor systems become more stringent. The increase in belt tension and the need for higher load-bearing capacities necessitate a shift toward precision-manufactured components that can maintain stability under extreme stress.
Procurement managers are advised to evaluate suppliers not just on initial cost, but on the total cost of ownership (TCO). Investing in high-specification components now reduces the frequency of emergency shutdowns, which are significantly more expensive than planned maintenance.
Real-world solutions for diverse material handling challenges.
Implementing high-tension belts and reinforced impact beds to handle large boulders and abrasive copper ore, reducing belt tears and improving uptime in the Copperbelt region.
Deploying specialized coal mine conveyor systems with flame-retardant components and integrated dust suppression to ensure safety in confined spaces.
Designing efficient transfer points using precision pulleys to move bulk minerals from rail to ship, minimizing material loss during the transition.
Installing low-noise, energy-efficient conveyor rollers for the continuous transport of limestone and clinker, optimizing power usage in industrial parks.
Using food-grade conveyor components for the movement of grain and maize, ensuring hygiene standards are met while maintaining high throughput speeds.
A journey of innovation in industrial conveying.
Established with a core focus on the design, manufacturing, and installation of bulk material handling and conveying equipment.
Expanded exports to over 40 countries, adapting manufacturing to comply with CEMA, DIN, JIS, and GB standards to serve diverse international markets.
Partnered with research institutes to develop energy-efficient and intelligent conveyor solutions, certified by ISO9001, CE, and SGS.
Precision components for maintaining maximum reliability in your transport ecosystem.
Expert answers to common procurement and technical questions.
Get professional engineering support for your industrial projects in Africa - Zambia. Let us help you build a reliable and efficient transportation ecosystem.
Discuss Your Requirements