Jun. 26, 2026
In the modern manufacturing landscape, the seamless movement of materials is the heartbeat of productivity. High-performance industrial conveyor systems are no longer just about moving items from point A to point B; they are about enhancing safety, reducing downtime, and maximizing throughput. For industries dealing with hazardous environments or heavy loads, choosing a system that integrates strength with specialized safety features—such as anti-static properties—is critical. This guide explores the technical advantages of premium conveyor solutions and how they transform material handling in demanding sectors.

Static electricity poses a significant risk in environments where combustible dust or flammable gases are present. To mitigate this, advanced industrial conveyor systems utilize specially formulated anti-static rubber compounds. These materials ensure that static charges are dissipated effectively, preventing sparks that could lead to catastrophic explosions. By integrating conductive properties into the belt's structure, operators can maintain a safe workflow in chemical plants and coal mines without compromising on speed or efficiency.
Safety Insight: Anti-static belts are essential for compliance with international safety standards in explosive atmospheres, ensuring a secure environment for both personnel and infrastructure.
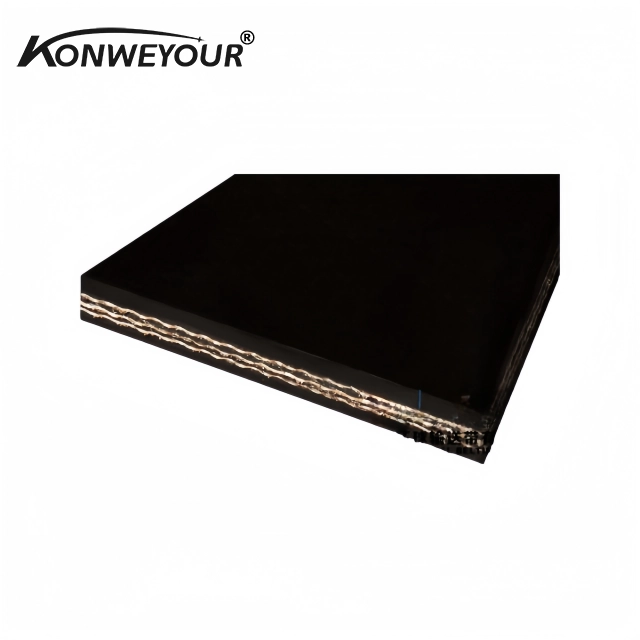
For long-distance transport of heavy materials, standard fabric belts often suffer from excessive elongation. This is where steel cord reinforced industrial conveyor systems provide a definitive advantage. By embedding high-tensile steel cords within the rubber matrix, these belts offer unmatched load-bearing capacity and low stretch. This stability ensures that the belt remains centered and maintains constant tension, which significantly reduces the energy required for propulsion and minimizes mechanical wear on the drive motors.
Choosing the right belt material is a strategic decision based on the specific demands of the application. While fabric belts are suitable for light-duty tasks, the rigorous demands of mining and heavy industry require the robustness of steel cords. The following comparison highlights why high-capacity industrial conveyor systems prioritize steel reinforcement for extreme environments.
The lifespan of industrial conveyor systems is primarily determined by the quality of the outer rubber covers. These covers must withstand constant abrasion from jagged ores, impact from heavy loads, and chemical aging. By using high-grade rubber compounds, belts can resist cuts and tears, significantly reducing the frequency of replacements. Furthermore, the strong adhesion between the steel cords and the rubber layers prevents delamination, ensuring the belt remains a single, cohesive unit even under extreme mechanical stress.

To ensure peak performance, it is essential to understand the technical parameters that define a high-quality conveyor belt. For those operating industrial conveyor systems in specialized sectors like power plants or chemical factories, optional flame resistance and specific conductivity levels are mandatory. Below are the standard specifications for our premium anti-static steel cord rubber belts:
The versatility of modern industrial conveyor systems allows them to be adapted for various heavy-duty environments. In coal mines, the combination of anti-static and flame-resistant properties is a legal and safety requirement to prevent underground disasters. In ports, steel cord belts handle massive volumes of bulk cargo over kilometers of distance with minimal sag. Similarly, chemical plants rely on these systems to move volatile materials safely. Regardless of the sector, the goal is to create a stable, reliable, and low-maintenance transport chain.
Choosing the right industrial conveyor systems is an investment in the long-term operational stability of your business. By integrating high-tensile steel cords with anti-static rubber technology, you ensure not only the safety of your workforce but also the efficiency of your material flow. Whether you are upgrading an existing facility or designing a new plant, prioritizing durability, conductivity, and strength will drastically reduce operational costs and risks. Trust in engineering excellence to keep your production moving forward.
Anti-static properties are crucial because the friction between the belt and the material, as well as the belt and the rollers, generates static electricity. In environments containing flammable dust or gases—such as coal mines or chemical plants—a static spark can trigger a devastating explosion. Anti-static belts use conductive rubber compounds to safely dissipate these charges to the ground, ensuring a safe working environment and compliance with strict industrial safety regulations.
Steel cord belts are designed for high-tension, long-distance, and heavy-load applications. Unlike fabric belts, which can stretch significantly under load, steel cords provide extreme tensile strength and very low elongation. This prevents the belt from sagging and reduces the need for frequent tension adjustments. While fabric belts are more flexible and cheaper for short, light-duty runs, steel cord belts offer a far longer lifespan and higher reliability in rigorous industrial conveyor systems.
Yes, most high-end conveyor belts can be customized to meet specific environmental needs. Flame-retardant grades are available to prevent the spread of fire in underground mines, while heat-resistant compounds are used in industries like cement or smelting where materials are transported at high temperatures. These customizations are achieved by altering the chemical composition of the rubber covers, ensuring that the belt maintains its structural integrity and safety features under extreme thermal stress.
The lifespan is primarily influenced by the abrasiveness of the material being transported, the impact force of the loading process, and environmental factors like UV exposure or chemical contact. Using a belt with a high-quality abrasion-resistant cover and ensuring proper alignment of the industrial conveyor systems prevents premature wear. Regular maintenance, such as checking for belt drift and cleaning debris from rollers, also significantly extends the operating life of the system.

Jun 22,26
High Performance Flame Retardant Conveyor Belt in Coal Mines
Feb 11,26
Find High Quality Conveyor Belt Rollers for Sale and Expert Guidance
Oct 27,25
Understanding Corrugated Sidewall Conveyor Systems for Efficient Material Handling
Efficient material transport is essential for industries such as mining, construction, agriculture, and bulk material handling.
Feb 14,26
Advanced Conveyor Construction Equipment for Modern Industrial Solutions

Jun 05,26
Engineering the Future of Aggregate Conveying Systems

Jun 21,26
High Quality Rubber Conveyor Rollers for Industrial Efficiency
SUBSCRIBE NEWSLETTER