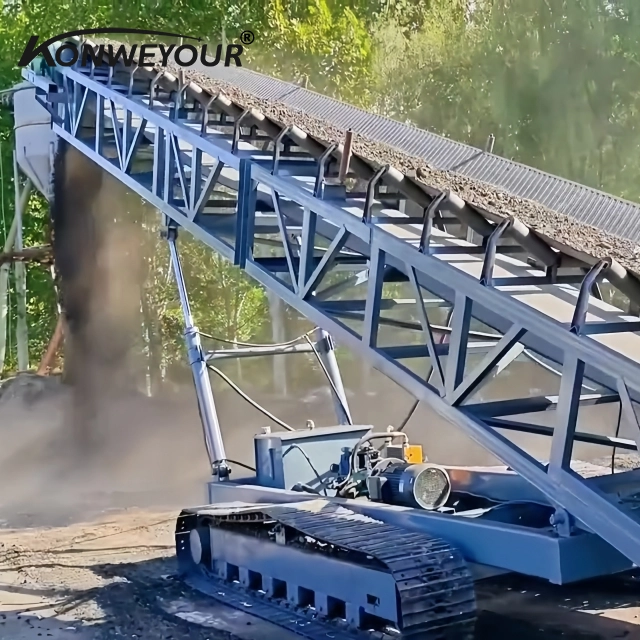



Integrating research and high-precision manufacturing to provide reliable transport support for mining and power plants.


Addressing the need for robust bulk handling in Rwanda's growing extractive and construction industries.
The industrial landscape in Rwanda is experiencing a steady transition towards modernized resource extraction and infrastructure development. For mining operations, the ability to move heavy volumes of ore efficiently is critical. Local enterprises often face the challenge of adapting equipment to varied terrain and specific mineral densities, requiring a mine conveyor that balances high load capacity with operational durability in diverse environments.
A significant pain point for Rwandan industrial operators is the wear and tear on moving parts due to abrasive materials. This creates a constant demand for high-quality conveyor components such as rollers and idlers that can withstand intense friction. Without standardized, certified parts, maintenance cycles become frequent and costly, leading to unplanned downtime in critical transport lines.
Looking forward, the integration of energy-efficient systems is becoming a priority. By adopting modular conveyor transfer systems, companies can optimize their flow paths and reduce energy consumption. The opportunity lies in moving from manual or fragmented transport to integrated, automated lines that comply with international standards like DIN or CEMA, enhancing overall productivity.
Tracing the shift from basic belt movement to intelligent, high-load industrial systems.
Focus on basic belt transportation with simple rollers, primarily used for short-distance material movement in early mining sites.
Introduction of specialized components and adherence to CEMA/DIN standards to handle higher tonnage and longer distances.
Shift toward energy-efficient, low-consumption ecosystems with smart monitoring and advanced wear-resistant materials.
Strategic directions for enhancing the reliability and efficiency of continuous conveying.
Increasing reliance on high-tolerance rollers and pulleys to minimize energy loss and eliminate belt misalignment.
Utilizing advanced composite materials for belt cleaners and impact beds to extend equipment lifespan in abrasive environments.
Adopting modular designs that allow for rapid expansion or reconfiguration as production volumes increase.
Ensuring all systems meet global safety and quality certifications (ISO, CE, SGS) to attract international investment.
The shift toward digitized material handling allows Rwandan operators to monitor system health in real-time. By analyzing tension and friction data, companies can move from reactive to predictive maintenance, significantly lowering operational risks.
Supply chain stability is equally vital. Sourcing components from manufacturers capable of meeting diverse international standards ensures that replacements are compatible and reliable, regardless of the original equipment brand.
Tailored conveyor solutions for various industrial and logistical applications.
Utilizing a specialized coal mine conveyor or ore system to transport raw materials from deep pits to processing plants, ensuring stability on steep inclines.
Implementing high-capacity belt systems for limestone and clinker transport, utilizing impact beds to protect the belt from heavy falling loads.
Deploying long-distance transfer systems for bulk cargo handling, focusing on high-efficiency pulleys to minimize energy costs during loading.
Continuous fuel feeding systems using precision rollers and cleaners to maintain a debris-free environment and ensure constant power output.
Light-to-medium duty conveyor systems for grains and coffee beans, focusing on hygienic materials and easy-to-clean components.
Hebei Juntong Machinery Manufacturing Co., Ltd.'s Global Journey
Company established with a dedicated focus on the design, manufacturing, and installation of bulk material handling and conveying equipment.
Launched self-developed high-performance conveyor systems, gaining strong domestic recognition for quality and operational reliability.
Began exporting to Southeast Asia, marking the first significant step towards becoming a global conveyor equipment supplier.
Implemented modernized production lines and advanced manufacturing technologies to increase annual capacity and efficiency.
Successfully exported products to Asia, Europe, Africa, and the Americas, establishing a trusted global footprint.
Continuous investment in eco-friendly and energy-efficient solutions to meet the evolving needs of clients worldwide.
From precision rollers to heavy-duty belt cleaners, find the exact specifications for your industrial ecosystem.
Expert answers to the most common questions regarding conveyor system implementation in Rwanda.
Leverage our global engineering expertise and certified manufacturing to build a low-consumption, high-reliability transport ecosystem for your business.
Request Custom Solution