Oct. 28, 2025
I’ve walked more dusty transfer houses than I care to admit, and the shift is obvious: plants are moving from open troughs to enclosed systems. The Enclosed Tubular Belt Conveyor sits right at that inflection point—less spillage, tighter footprints, cleaner air. To be honest, once you’ve seen a decent install run through a rainy season without a single housekeeping panic, it’s hard to go back.
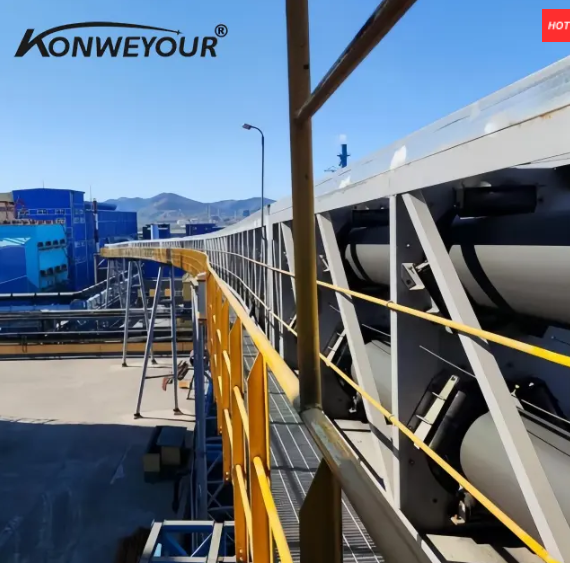
Three macro drivers keep coming up in my notes: ESG-driven dust abatement, labor shortages (less cleanup), and site constraints around ports and brownfield expansions. Enclosed conveyors—tubular or “pipe”—solve for all three, while sidestepping some permitting headaches. In fact, many customers say they adopted them just to keep neighbors happy.
| Capacity | ≈ 30–800 t/h (real-world use may vary with material & slope) |
| Tube diameter | ≈ 150–500 mm |
| Belt speed | ≈ 1.5–4.0 m/s |
| Max incline | up to ~25° (material dependent) |
| Curve radius (horizontal) | ≈ 300–600 m |
| Particle size | ≤ 80 mm (soft) / ≤ 40 mm (abrasive) |
| Dust emissions | < 10 mg/m³ at discharge with proper filtration (site-tested) |
| Ambient temp | -20 to +50 °C standard; options to -40/+80 °C |
Ports and grain terminals, cement and clinker lines, fertilizer and potash, coal/coke (with proper sealing), battery metals concentrates, and—surprisingly—sugar and malt where hygiene and cross-contamination are touchy subjects.
Materials: EP/ST belts with anti-tear layers; idlers in hexagonal sets; sealed feed chutes with wear liners (AR, ceramic, or UHMW).
Methods: DIN 22101/ISO 5048 power & tension calcs; finite-element checks on gantries; hot-vulcanized splices where feasible.
Testing: belt abrasion (ISO 4649), elongation (ISO 283), idler runout/noise, factory run-in; dust verification against local limits.
Service life: belt 3–7 years typical; idlers 20–40k h; bearings L10 ≥ 50k h with proper sealing and alignment.
| Vendor | Tube dia. | Capacity | Certs | Lead time | Notes |
|---|---|---|---|---|---|
| JTC Conveyor (Hebei; No. 13 Gongqiang Rd., Nangong E.D.Z.) | 150–500 mm | 30–800 t/h | ISO 9001, CE; ATEX options | ≈ 10–16 weeks | Strong customization, competitive CAPEX |
| Global Brand A (pipe conveyor) | 200–600 mm | 100–1200 t/h | ISO, CE, regional | ≈ 20–30 weeks | Premium lifecycle services |
| Regional Fabricator B | 150–400 mm | 50–400 t/h | CE (varies) | ≈ 8–14 weeks | Cost-effective, limited curve expertise |
Enclosed Tubular Belt Conveyor options include anti-abrasive and heat-resistant belts (ISO 14890), food-grade compounds, stainless or polymer idlers, ceramic-lined chutes, drive station redundancy, ATEX/IECEx electricals for Zone 21/22, condition monitoring (idler acoustics, belt drift sensors), and quick-access inspection doors. I guess the right mix depends on what you’re moving and how picky your insurer is.
Designed and verified per DIN 22101 and CEMA; belt specs per ISO 14890; power calcs per ISO 5048. Dust controls aligned with OSHA grain handling and NFPA 652 guidance; ATEX 2014/34/EU packages available. Field sound levels typically ≤ 75 dB(A) at 1 m with guard sealing, though, yes, real plants vary.
Feedback from users: “Cleaner yard, fewer complaints,” and “maintenance got boring—in a good way.” If you know, you know.
References

Jun 27,26
Efficient Industrial Powered Roller Conveyor System Solutions
Mar 07,26
Optimizing Material Handling Systems with Durable Conveyor Roller Shafts

Aug 17,26
Top Conveyor Belt Company Providing Spiral Cage Pulleys
Jun 25,25
Multi-Standard System Enhances Mining Port Efficiency
Today, Hebei Juntong Machinery Manufacturing Co., Ltd. officially launched the "MRT Pro" series intelligent belt conveyor system

Sep 17,26
Technical Guide to Optimizing Factory Conveyor Systems
Dec 03,25
Comprehensive Guide to Conveyor Belt System Parts – Industry & Global Applications
SUBSCRIBE NEWSLETTER