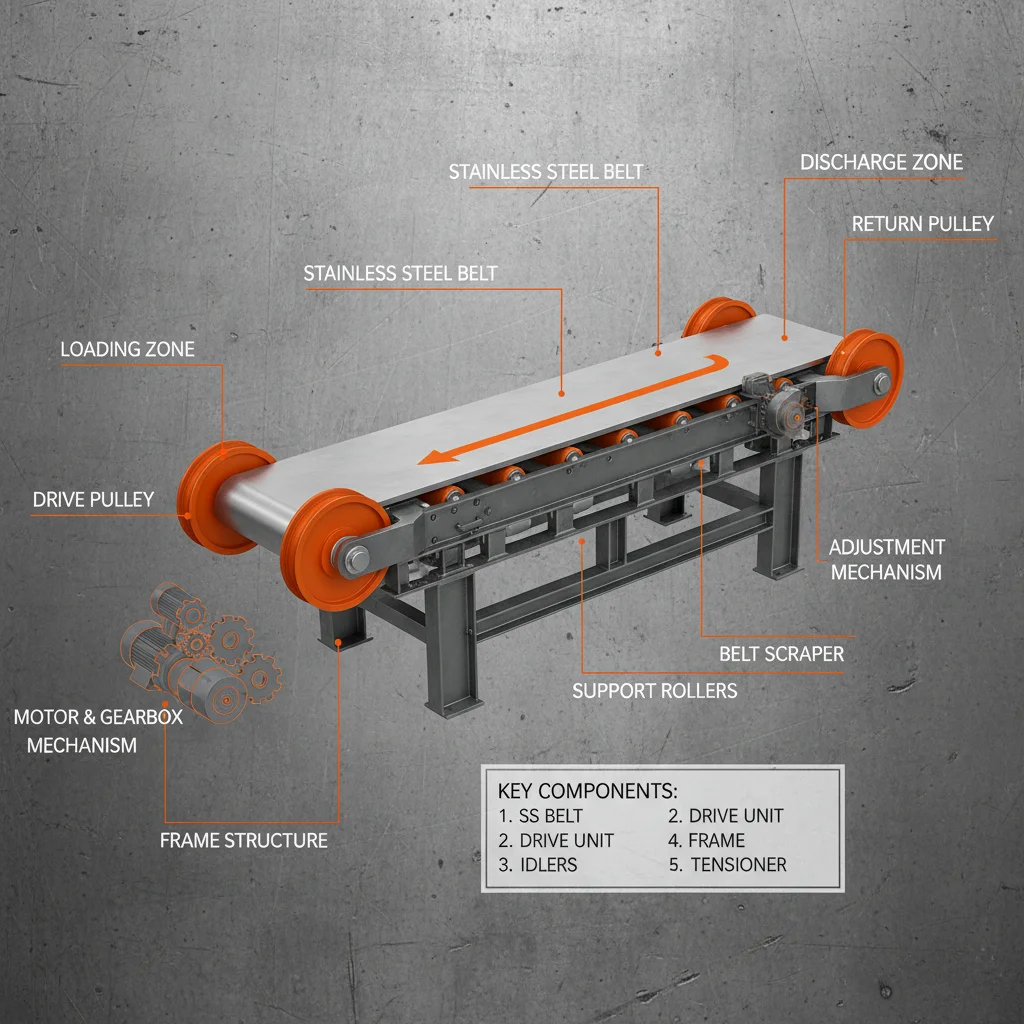
Belt slippage in heavy-duty industrial settings is more than a minor inefficiency; it is a primary driver of premature component wear and unplanned downtime. In facilities where bulk material transport is constant, the interface between the drive pulley and the belt determines the overall stability of the entire transport chain.
The challenge arises when environmental contaminants—such as moisture, dust, or abrasive debris—compromise the friction coefficient of standard rubber lagging. This often leads to power transmission losses and an increased risk of belt damage, forcing operators to choose between frequent maintenance cycles or reduced operational speeds.
Addressing these bottlenecks requires a shift toward high-traction engineering. By optimizing the conveyor belt in factory environments through advanced material integration, such as ceramic lagging, industries can significantly extend equipment life and energy efficiency.


In many mining and cement facilities, the drive pulley is the most stressed point of the system. Standard rubber lagging often fails under extreme abrasion, leading to a "glazing" effect where the rubber becomes smooth and loses its grip. This failure results in the belt sliding over the pulley, which generates heat and accelerates the degradation of the belt's bottom cover.
This inefficiency is not just a maintenance issue but a financial one. Energy is wasted as the motor works harder to overcome slippage, and the resulting downtime for relagging can halt entire production lines. The transition to ceramic-enhanced surfaces addresses these fundamental physics of friction and wear.
The Engineering Grade Ceramic Lagging Drive Pulley utilizes a synergistic construction. It embeds high-alumina ceramic tiles within a premium rubber matrix. This design leverages the extreme hardness of ceramics to resist abrasion while the rubber provides the necessary elasticity to absorb shock loads and maintain a tight seal against the belt.
Unlike traditional coatings, the ceramic tiles are precision-embedded to ensure they do not detach under high shear stress. This prevents the pulley surface from becoming uneven, which would otherwise cause belt tracking issues and uneven wear across the belt width. The resulting surface maintains a consistent coefficient of friction even in wet or oily conditions.
Furthermore, the lagging process—whether through hot vulcanization or cold bonding—is critical. Hot vulcanization, in particular, creates a permanent chemical bond between the rubber matrix and the steel shell of the pulley, ensuring that the lagging does not peel away during heavy-duty startup and braking cycles.
Beyond the surface lagging, the internal architecture of a drive pulley must withstand immense torsional forces. The use of Q355B seamless steel tubes for the shell and 42CrMo alloy steel for the shafts provides the necessary yield strength to prevent deflection under full load.
Reliability in bulk material handling is achieved not by over-engineering a single part, but by ensuring the structural integrity of the shaft and shell through rigorous Non-Destructive Testing (NDT), including ultrasonic and X-ray flaw detection.
Precision machining and heat treatment (reaching HB 217-286) ensure that the bearing seats and shaft ends are perfectly aligned. This reduces vibration and prevents the premature failure of self-aligning roller bearings from brands like SKF or FAG, which are essential for maintaining smooth rotation in contaminated industrial environments.
When comparing standard rubber lagging to ceramic lagging, the most immediate difference is observed in the traction-to-wear ratio. Rubber provides excellent initial grip but degrades rapidly in abrasive environments. Ceramic lagging maintains a high friction coefficient over a significantly longer period, effectively eliminating the "slippage window" that occurs as rubber wears down.
This performance gap is most evident when evaluating power transmission efficiency. By eliminating slippage, the drive pulley ensures that nearly 100% of the motor's torque is transferred to the belt, reducing energy consumption and preventing the overheating of the belt carcass.
In a typical quarrying operation, the conveyor system is exposed to constant dust and moisture. Here, a standard pulley often struggles with "wet slip," where a thin layer of water and fines creates a lubricating film between the rubber and the belt. The Engineering Grade Ceramic Lagging Drive Pulley solves this by using the hard edges of the ceramic tiles to "cut through" the contaminant layer, maintaining direct contact with the belt.
Similarly, in cement plants where high loads are intermittent, the shock-absorbing rubber matrix protects the pulley core from impact loads during sudden startups. This combination of hardness for grip and elasticity for protection makes it an essential component for any high-capacity bulk material transport system.
The industry is moving away from a "lowest initial cost" procurement model toward a "Total Cost of Ownership" (TCO) approach. Operators have realized that while ceramic lagging pulleys have a higher upfront investment, the drastic reduction in replacement frequency and energy costs creates a far superior return on investment.
We are also seeing a trend toward intelligent monitoring. By combining high-durability components with sensors that detect belt slip in real-time, factories can optimize their load distribution and further extend the life of their conveyor systems. This integration of material science and digital monitoring is the current frontier of bulk handling.
As global standards like CEMA and DIN evolve, there is an increasing emphasis on zero-defect structural integrity. This has made advanced NDT (Non-Destructive Testing) a standard requirement rather than an optional add-on, ensuring that the internal shaft can handle the increased torque provided by higher-friction lagging.
Choosing the right drive pulley requires balancing material requirements against operational stresses. The decision typically hinges on the primary failure mode of the existing system: is it surface wear, structural deflection, or bearing failure?
For environments with extreme abrasion, ceramic lagging is the only viable long-term solution. However, for lighter applications, diamond or chevron patterns may suffice. The key is to match the lagging hardness (e.g., 65±5 Shore) and the shaft material (Carbon vs. Alloy steel) to the specific tonnage and speed of the conveyor.
The following framework provides a relative assessment of different pulley configurations based on typical industrial requirements.
| Lagging Type | Wear Resistance | Traction Level | Ideal Application |
|---|---|---|---|
| Standard Rubber | Low to Medium | Moderate | Light Industrial/Dry |
| Ceramic Lagging | Extreme | Superior | Mining/Cement/Wet |
| Diamond Pattern | Medium | High | General Bulk Handling |
| Chevron Pattern | Medium | High (Self-Cleaning) | Sticky Materials |
| Urethane | Medium | Moderate | Chemical/Food Grade |
| Herringbone | Medium | High | Moderate Load Transport |
Ceramic lagging combines the hardness of ceramic tiles with the flexibility of rubber. In mining, where abrasive materials and moisture are prevalent, rubber wears down quickly and loses grip. Ceramic tiles resist this abrasion and maintain a high friction coefficient, which eliminates belt slippage and significantly extends the service life of both the pulley and the conveyor belt.
The shaft bears the entire torsional load of the conveyor. Using high-grade alloy steels like 42CrMo instead of basic carbon steel prevents shaft deflection and fatigue. When combined with precise heat treatment and ultrasonic flaw detection, the shaft can withstand extreme industrial loads without developing structural cracks, ensuring long-term operational stability.
Hot vulcanization creates a permanent chemical bond between the lagging material and the steel shell, making it far more resistant to peeling under high shear stress. Cold bonding is faster and more convenient for on-site repairs, but for new, heavy-duty drive pulleys, hot vulcanization is recommended to ensure maximum bonding strength and durability.
While ceramic lagging is highly versatile, the specific pattern and hardness should be matched to the belt's cover material. Most industrial-grade belts are compatible, but for specialized belts, customization of the lagging pattern (such as Diamond or Chevron) may be necessary to optimize the grip and prevent premature wear of the belt's bottom cover.
Advanced sealing systems create a physical barrier that prevents dust, moisture, and chemical contaminants from entering the bearing housing. Since drive pulleys often operate in harsh environments, these seals protect the lithium-based grease and the roller bearings from contamination, which prevents overheating and unplanned bearing failure.
The ROI is realized through three primary channels: reduced replacement frequency (longer service life), lower energy costs (elimination of slippage), and decreased unplanned downtime. While the initial cost is higher, the total cost of ownership is significantly lower over a 3-to-5-year period compared to standard rubber pulleys.
The efficiency of a conveyor belt in factory environments depends heavily on the reliability of its drive components. By moving toward engineering-grade ceramic lagging and high-strength alloy constructions, industrial operators can effectively eliminate the costly cycle of slippage and premature wear.
As material handling demands increase, the integration of precision-engineered pulleys and rigorous quality control—such as NDT and specialized heat treatments—will remain the gold standard for ensuring high-uptime, energy-efficient transportation systems in the most demanding industrial sectors.
SUBSCRIBE NEWSLETTER